Unconfigured Ad Widget

Collapse

Laugh at my learning curve

Collapse
X
 
  • Time
  • Show
Clear All
new posts
  • Experimentalist
    Banned in Amsterdam
    CGN Contributor - Lifetime
    • May 2006
    • 1171

    Laugh at my learning curve

    I've been tinkering with 1911 pistols of late, learning how the firearm functions and doing some basic upgrades. Recently I thought I'd try my hand at so called "Dragon Scale" type texturing. I like what I've seen online and figured it can't be that difficult...

    First task was to sit down and do the geometry. How far do I want to cut into the slide, what angle does the slide need to be presented to the cutting tool (my mill does not tram), etc.

    Once I got everything worked out I wrote some CNC code and verified function on a piece of wood. My operating theory is it's best to make mistakes on cheap wood first and save the expensive metal. The wood test cuts came out nicely, I was quite happy with the uniformity of the pattern and the overall appearance. So time to move on to the metal.

    The photo below is how it turned out on the first side (the left side). The cuts started out on the shallow side and got shallower from there - I guess Springfield MilsSpec slides aren't too flat.

    IMG_1612.jpg

    What you see in the above photo isn't the original pattern, I spent a couple hours struggling to improve the results.

    For the right side of the slide I was more careful to measure the slope of the slide in the region into which the Dragon Scale was to be engraved. The results are certainly more uniform.

    IMG_1616 rotated.jpg

    I am presenting the slide at approximately 25 degrees from horizontal, and am thinking this may be a little too steep. Again, it looked great in the wood, less so here. Spindle is spinning at 2090 RPM using a 4 flute HSS bit at a plunge rate of 0.7 ipm.

    My primary lessons are:
    1) Springfield MilSpec slides aren't too flat.

    2) Take care to ensure the part is correctly aligned in the locality you're working in, not relying upon whole-part measurements.

    3) Be more careful to ensure the cuts don't go beyond the flat of the slide. When I originally did the geometry I figured the curves of the slide would be forgiving of cuts that weren't directly over the flat. Experience shows that was wrong - at least along the upper edge of the pattern (yuck!).

    A question to the group: I presume slides from other manufacturers are easier to work with. Any suggestions from whom I should order?

    Other thoughts, hints, and tips would be much appreciated.
    "An unarmed man can only flee from evil. And evil is not overcome by fleeing from it" - Col. Jeff Cooper

    "Shot placement trumps all."

    Originally posted by CSACANNONEER
    Who uses 9mm for SD? Anything less than a 50BMG is stupid to use. Personally, I prefer canister rounds out of a 10lb Parrott rifle for SD.
  • #2
    lamduh
    Senior Member
    • Dec 2011
    • 1964

    I cant really help in the maching part but that right side looks like your moving in the right direction. As for the slides i would try fusion firearms or heavy armory division and get some blank slides before moving on to Caspian or higher end brands first. Atleast you won't break the bank during trial and error phase.

    Sent from my SM-N950U using Tapatalk

    Comment

    • #3
      Experimentalist
      Banned in Amsterdam
      CGN Contributor - Lifetime
      • May 2006
      • 1171

      Originally posted by lamduh
      I cant really help in the maching part but that right side looks like your moving in the right direction. As for the slides i would try fusion firearms or heavy armory division and get some blank slides before moving on to Caspian or higher end brands first. Atleast you won't break the bank during trial and error phase.

      Sent from my SM-N950U using Tapatalk
      Thanks for the suggestion, was considering Fusion Firearms.

      Looking at the work under a magnifying viewer, it seems there are some areas that are not getting milled. The angle is so steep that the bit is leaving some of the original flat from the side of the slide. It looked fine in wood, but in metal it's just not right. I'm going to try a shallower angle, such that the end mill will create full circles in the slide. Subsequent rows will stair-step along, creating the desired pattern.
      Last edited by Experimentalist; 07-05-2020, 6:21 PM.
      "An unarmed man can only flee from evil. And evil is not overcome by fleeing from it" - Col. Jeff Cooper

      "Shot placement trumps all."

      Originally posted by CSACANNONEER
      Who uses 9mm for SD? Anything less than a 50BMG is stupid to use. Personally, I prefer canister rounds out of a 10lb Parrott rifle for SD.

      Comment

      • #4
        smoothy8500
        Veteran Member
        • Sep 2009
        • 3846

        Looks good enough and is functional. Bead-blast and blue/parkerize.

        Comment

        • #5
          NeilMo
          Member
          • Nov 2018
          • 356

          Originally posted by Experimentalist
          A question to the group: I presume slides from other manufacturers are easier to work with. Any suggestions from whom I should order?

          Other thoughts, hints, and tips would be much appreciated.


          You're off to a great start, congrats. Only one way to learn and that's to dive right in. Sarco has cheap castings that you can do lots to and not break the bank.

          Slide
          Frame

          Comment

          • #6
            The War Wagon
            I need a LIFE!!
            • Apr 2011
            • 10294

            Sharper than I could do - EITHER side!
            sigpic

            Comment

            • #7
              ar15barrels
              I need a LIFE!!
              • Jan 2006
              • 57174

              Originally posted by Experimentalist
              I am presenting the slide at approximately 25 degrees from horizontal, and am thinking this may be a little too steep.

              My primary lessons are:
              1) Springfield MilSpec slides aren't too flat.

              2) Take care to ensure the part is correctly aligned in the locality you're working in, not relying upon whole-part measurements.

              3) Be more careful to ensure the cuts don't go beyond the flat of the slide. When I originally did the geometry I figured the curves of the slide would be forgiving of cuts that weren't directly over the flat. Experience shows that was wrong - at least along the upper edge of the pattern (yuck!).

              A question to the group: I presume slides from other manufacturers are easier to work with. Any suggestions from whom I should order?

              Other thoughts, hints, and tips would be much appreciated.
              First off, the slide should be indicated flat to the mill table and the head should be kicked over to give the angle.
              This will ensure that the depth of cut is the same in all locations.
              If the slide is not flat, start out by making it flat before you even fixture it.
              Then, you will see that it's flat while indicating it in the vise.
              Randall Rausch

              AR work: www.ar15barrels.com
              Handguns: www.handgunbarrels.com
              Bolt actions: www.700barrels.com
              Foreign Semi Autos: www.akbarrels.com
              Most work done while you wait on a scheduled shop visit.

              Comment

              • #8
                ar15barrels
                I need a LIFE!!
                • Jan 2006
                • 57174

                Originally posted by lamduh
                At least you won't break the bank during trial and error phase.
                Trial and error should all be worked out before cutting on expensive parts.
                A piece of similar alloy metal bar with similar hardness is ideal.
                Randall Rausch

                AR work: www.ar15barrels.com
                Handguns: www.handgunbarrels.com
                Bolt actions: www.700barrels.com
                Foreign Semi Autos: www.akbarrels.com
                Most work done while you wait on a scheduled shop visit.

                Comment

                • #9
                  Experimentalist
                  Banned in Amsterdam
                  CGN Contributor - Lifetime
                  • May 2006
                  • 1171

                  Originally posted by ar15barrels
                  First off, the slide should be indicated flat to the mill table and the head should be kicked over to give the angle.
                  This will ensure that the depth of cut is the same in all locations.
                  If the slide is not flat, start out by making it flat before you even fixture it.
                  Then, you will see that it's flat while indicating it in the vise.
                  Hi Randal, thanks for the feedback. If my mill head could kick over, I agree that would certainly be my preferred method. Unfortunately it is fixed, and my only recourse is to tilt the work piece.

                  I use angle blocks to get me into the ballpark. After my experience with the left side I stopped relying on the angle blocks and took greater pains to place the local area at the correct angle. This was done by measuring heights at both ends, tapping the work piece with a hammer to adjust, then repeat. Then realize the angle changes just a little bit when you cinch up the vise, so iterate some more...

                  But you make an excellent point, facing the slide side helps not only with variability in the side height (relative to the mill table) but also in ensuring that subsequent placement using angle blocks will give a more correct angle to the work piece.

                  Thanks for the advice.
                  "An unarmed man can only flee from evil. And evil is not overcome by fleeing from it" - Col. Jeff Cooper

                  "Shot placement trumps all."

                  Originally posted by CSACANNONEER
                  Who uses 9mm for SD? Anything less than a 50BMG is stupid to use. Personally, I prefer canister rounds out of a 10lb Parrott rifle for SD.

                  Comment

                  • #10
                    Experimentalist
                    Banned in Amsterdam
                    CGN Contributor - Lifetime
                    • May 2006
                    • 1171

                    Originally posted by smoothy8500
                    Looks good enough and is functional. Bead-blast and blue/parkerize.
                    Originally posted by NeilMo
                    You're off to a great start, congrats. Only one way to learn and that's to dive right in. Sarco has cheap castings that you can do lots to and not break the bank....
                    Originally posted by Vertigofirearms
                    Looks nice
                    Originally posted by The War Wagon
                    Sharper than I could do - EITHER side!
                    Thanks guys. In addition to seeking advice I was hoping to illustrate my learning process. Hopefully with a little patience, some good advice, and properly learned technique this thread will culminate in something that I can be proud of.

                    Too often we get to see the edited results of a process, not the mistakes done along the way. Granted, I'm very new and these are base rookie errors. But I do hope they help others to avoid my silly mistakes. And maybe it will help some to not feel so bad when their efforts fall short of the artwork we usually get to see. I'm confident I'll eventually get there. Thank you to the teachers and cheer leaders who help along the way.

                    This is one of the reasons the TV show "Forged in Fire" is my favorite. I'm not a bladesmith; the only things I know of the process I learned from watching the show. But I really enjoy watching people practice their art. And in the demanding contest environment even the best sometimes come up short. I don't enjoy seeing people suffer or struggle, I'm cheering them on from my couch. But I do appreciate an honest show that shows not only the triumphs, but also the struggles that are the cost of admission.
                    "An unarmed man can only flee from evil. And evil is not overcome by fleeing from it" - Col. Jeff Cooper

                    "Shot placement trumps all."

                    Originally posted by CSACANNONEER
                    Who uses 9mm for SD? Anything less than a 50BMG is stupid to use. Personally, I prefer canister rounds out of a 10lb Parrott rifle for SD.

                    Comment

                    • #11
                      ar15barrels
                      I need a LIFE!!
                      • Jan 2006
                      • 57174

                      Originally posted by Experimentalist
                      If my mill head could kick over, I agree that would certainly be my preferred method.
                      Unfortunately it is fixed, and my only recourse is to tilt the work piece.
                      That's your main problem.
                      See what it will take to turn your head.
                      Maybe make a new column or a system with an angle block.
                      If your Z axis movement is in the spindle, you don't need the be able to slide the head up and down on your job specific head mount.
                      You could probably make a custom head mount that is stiffer than the existing column.

                      Next is that if you are stuck with tilting the part, you will get better results with the endmill by cutting with the side, not the end.
                      When the part is tilted, you can mill each cut as an X cut instead of as a Z plunge.
                      Last edited by ar15barrels; 07-06-2020, 12:31 PM.
                      Randall Rausch

                      AR work: www.ar15barrels.com
                      Handguns: www.handgunbarrels.com
                      Bolt actions: www.700barrels.com
                      Foreign Semi Autos: www.akbarrels.com
                      Most work done while you wait on a scheduled shop visit.

                      Comment

                      • #12
                        Experimentalist
                        Banned in Amsterdam
                        CGN Contributor - Lifetime
                        • May 2006
                        • 1171

                        Okay, moving in the right direction

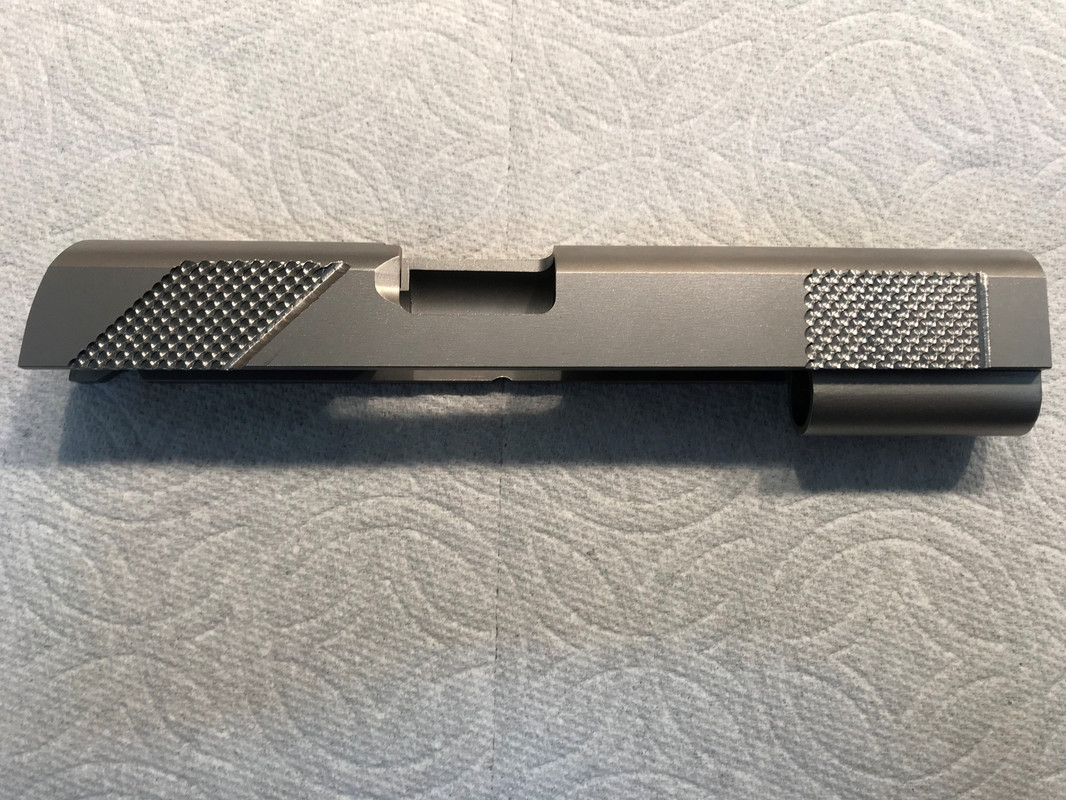
                        Hi everyone. Thought I'd post up some pictures of my latest "Dragon Scale" patterning efforts.

                        I cleaned up the extra pattern elements that were too high (and thus marring the slide), reduced the angle to 10 degrees (from the previous 25 degrees), and took care to ensure the slide was both at the correct angle in the "X" coordinate direction, and "flat" in the Y coordinate direction.


                        I'm still using angle blocks to orient the slide in the milling vise. I've improved accuracy by placing a parallel block flat along the bottom, bridging the flexible center. The angle block goes on top of that, with the slide on top. Checking the angle it comes out to within a thousandth or two in a two inch run in "X" coordinate. Close enough for Rock 'n Roll.

                        I found that the slide wasn't flat in the Y coordinate direction (bottom to top in the picture) when initially placed into the vise, so used 0.010" and 0.020" shim stock to fix the problem.

                        It's a slide from Fusion Firearms. Nice and pretty from the manufacturer, I almost felt bad cutting into it. But the results here make me pretty happy. Took a month or so for the slide to arrive, Fusion Firearms was (and presumably still is) pretty slammed. As are all retailers in the firearms industry, it's going to be an interesting ride the next couple years. But I digress.
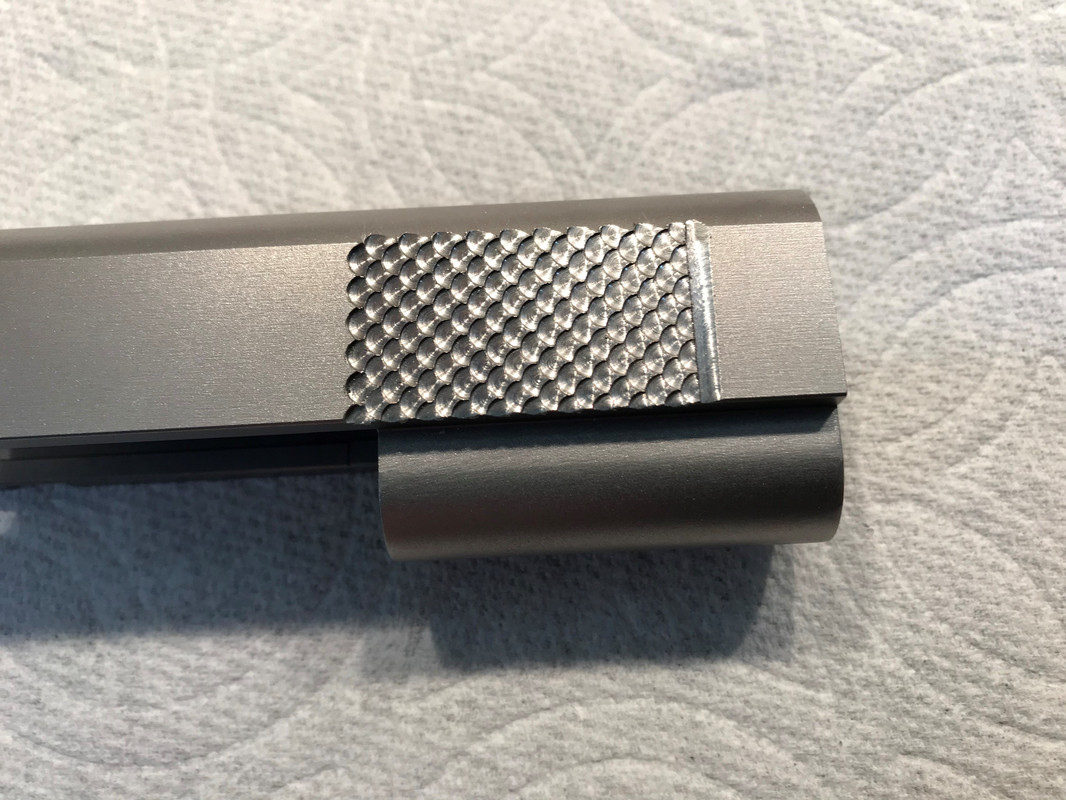
                        Here are some close up shots. I know the aft end photo is blurry, sorry about that.


                        The clean up cut at the front of the rear diagonal pattern was interesting to set up. It's a straight line cut, angled in all three dimensions since the slide is at a 10 degree angle in the Z axis, and the cut moves diagonally in the X-Y plane. I did the geometry, figuring out where I needed to start and where I needed to end up. Then used a "G01" command to set up the cut. It worked out pretty well, methinks.

                        I've only done the right side so far, the left side remains undone. I try to only tinker when I'm feeling fresh and enthusiastic. I had made several trial cuts in wood, did a fair bit of math, verified that math in wood, then did the aft end of the slide today. When I get tired I start to make mistakes. So, it was time to clean up the mill, come inside and do something else.

                        Thanks for looking.
                        "An unarmed man can only flee from evil. And evil is not overcome by fleeing from it" - Col. Jeff Cooper

                        "Shot placement trumps all."

                        Originally posted by CSACANNONEER
                        Who uses 9mm for SD? Anything less than a 50BMG is stupid to use. Personally, I prefer canister rounds out of a 10lb Parrott rifle for SD.

                        Comment

                        • #13
                          mtenenhaus
                          Veteran Member
                          • Jul 2007
                          • 3416

                          I recall watching a very well known gunsmith checker...he spent a lot of time recontouring the frame prior to any work...it wouldn't have occurred to me had i not seen that before.

                          With respect to the Springfield slide, do you think the texturing on the rounded (top) aspect of the slide might be ameliorated by recontouring the rounded section?

                          Comment

                          • #14
                            Experimentalist
                            Banned in Amsterdam
                            CGN Contributor - Lifetime
                            • May 2006
                            • 1171

                            Originally posted by mtenenhaus
                            I recall watching a very well known gunsmith checker...he spent a lot of time recontouring the frame prior to any work...it wouldn't have occurred to me had i not seen that before.

                            With respect to the Springfield slide, do you think the texturing on the rounded (top) aspect of the slide might be ameliorated by recontouring the rounded section?
                            You make a good point, some judicious work with a file and sandpaper likely would take care of those errant marks.

                            The sparse pattern on the left side might be harder to repair. The cuts are fairly deep, might try cleaning them off completely with a facing operation and then... Maybe some engraving cuts?

                            Now you have me thinking... Thanks.
                            "An unarmed man can only flee from evil. And evil is not overcome by fleeing from it" - Col. Jeff Cooper

                            "Shot placement trumps all."

                            Originally posted by CSACANNONEER
                            Who uses 9mm for SD? Anything less than a 50BMG is stupid to use. Personally, I prefer canister rounds out of a 10lb Parrott rifle for SD.

                            Comment

                            • #15
                              mtenenhaus
                              Veteran Member
                              • Jul 2007
                              • 3416

                              One other possible consideration if you're not happy with the current design

                              ....take a peak at the FN Hi-Power pistol.

                              ....you might be able to contour down the sides to simulate that look


                              Bud's Gun Shop - Your trusted source for firearms, ammunition, and accessories. Shop our extensive selection of guns, ammo, optics and more.
                              Last edited by mtenenhaus; 09-22-2020, 11:15 PM.

                              Comment

                              Working...
                              UA-8071174-1